
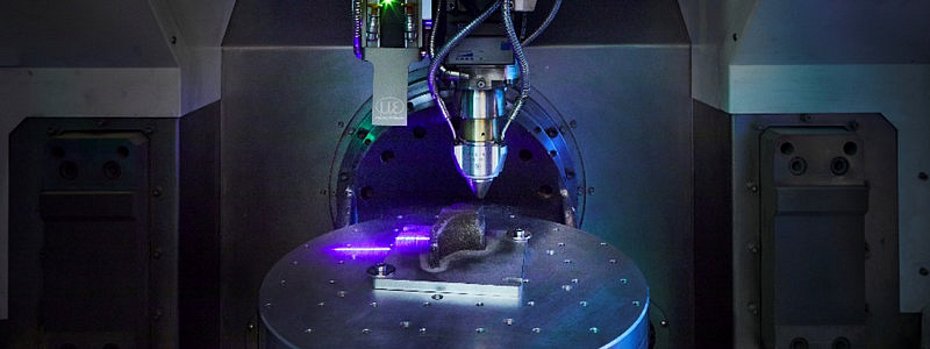
The proper manufacture and maintenance of die-casting tools is of central importance to the foundry industry: As one of the most expensive assets, they play a decisive role in determining quality, efficiency, and cost-effectiveness. Complex molds and inserts can easily cost hundreds of thousands of euros, and their unrestricted functionality is essential for production over many years. They must withstand extreme stresses. In die casting, temperatures of up to 700 °C act on the mold material, while the dies are simultaneously exposed to mechanical forces of several hundred kilonewtons. Added to this are abrasive stresses on the mold surface and chemical corrosion caused by alloying elements in the cast materials. Thermal stresses and material fatigue lead to cracking, erosion, and abrasive wear. Even with optimal design and careful manufacturing of the molds, their wear is an unavoidable factor that eventually necessitates tool replacement. If this occurs unexpectedly, it results in high follow-up costs.
Laser Cladding for More Durable Die-Casting Molds
The economic impact is significant: Every tool failure results in production downtime, additional setup times, and sometimes the need to manufacture new inserts or even entire tools. Added to this is the growing pressure to manufacture and operate molds in a way that is not only cost-effective but also sustainable. ““In an industry where every minute of production time counts, we need processes that can extend tool lifecycles, reduce downtime, and optimize production processes from an environmental perspective,” explains Dr. Thomas Schopphoven, head of the Laser Cladding Department at the Fraunhofer Institute for Laser Technology ILT in Aachen. Traditional approaches, such as the use of high-alloy tool steels, are reaching their physical limits. Higher hardness and wear resistance often mean complex processing, long lead times, and high raw material costs. In addition to service life considerations, demands for flexibility in tool manufacturing are also increasing: Product modifications regularly require changes to mold inserts, sprue, and cooling systems, which pose additional challenges for toolmakers.
The search for solutions must therefore go beyond existing strategies. Conventionally, tools are made of a single material, which limits their performance and makes them difficult to repair. Innovative manufacturing technologies such as Laser Material Deposition (LMD) not only enable the repair of tools but also the selective coating of areas subject to particularly high stress, as well as the flexible adaptation of geometries through hybrid additive manufacturing approaches. In this way, molds can be used longer, adapted more quickly, and operated in a more resource-efficient manner. At a time when the circular economy is gaining increasing importance even in industrial toolmaking, this technology offers enormous forward-looking potential.
Laser Material Deposition and EHLA
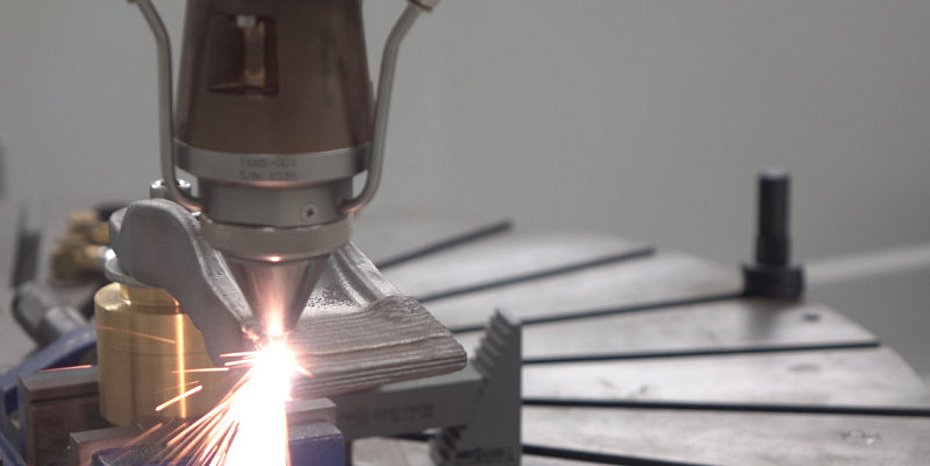
Laser material deposition, often referred to as laser cladding, is an additive manufacturing process that has become widely used in industry across numerous sectors, such as the repair of turbomachinery components or the coating of rollers and cylinders. The principle is simple; the possibilities are remarkable. A laser beam creates a molten pool of precisely controllable size on the surface of a workpiece, while metal powder is simultaneously fed into this molten pool. Through precise control of the travel paths, material is deposited locally, layer by layer, which not only rebuilds worn areas but also allows for the creation of new, functional geometries. What sets this process apart is its high level of process control: laser parameters, powder feed, and feed rate are precisely coordinated so that heat input remains minimal and thermal stresses are reduced.
A further development of this process is the multi-award-winning Extreme High-Speed Laser Cladding (EHLA), which Dr. Schopphoven developed several years ago at Fraunhofer ILT: “While conventional LMD is primarily used for thicker layers in the millimeter range, EHLA allows for the production of very thin, wear-resistant coatings with layer thicknesses starting at approximately 30 µm.” This is achieved at a speed that truly lives up to the process’s name: speeds of several hundred meters per minute are possible. The technology is now well established in numerous industries; several hundred EHLA systems are already in industrial use worldwide. The key advantage lies in precision and efficiency: EHLA makes it possible to process even material combinations that are difficult to weld—such as high-alloy tool steels or cemented carbides—reliably while maintaining low energy consumption. With EHLA3D, the process reaches a new level. Through integration into 5-axis CNC machines, the technology can be used not only for coatings and minor repairs but also for additive manufacturing. Complex free-form geometries can thus be built up on semi-finished products with high precision to the final contours. In this way, the technology combines capabilities from the fields of manufacturing, coating, and repair into a single process that can be used both for the production of new tools and for their regeneration. Of particular interest to toolmaking is the ability to selectively reinforce functional zones without having to remanufacture the entire tool. The low heat input allows for the machining of sensitive geometries without warping, while the high deposition rate enables cost-effective production even on large surfaces.
Benefits for the Foundry Industry
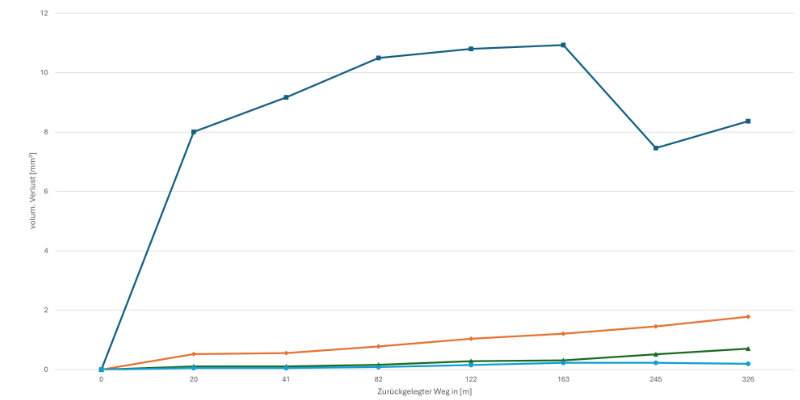
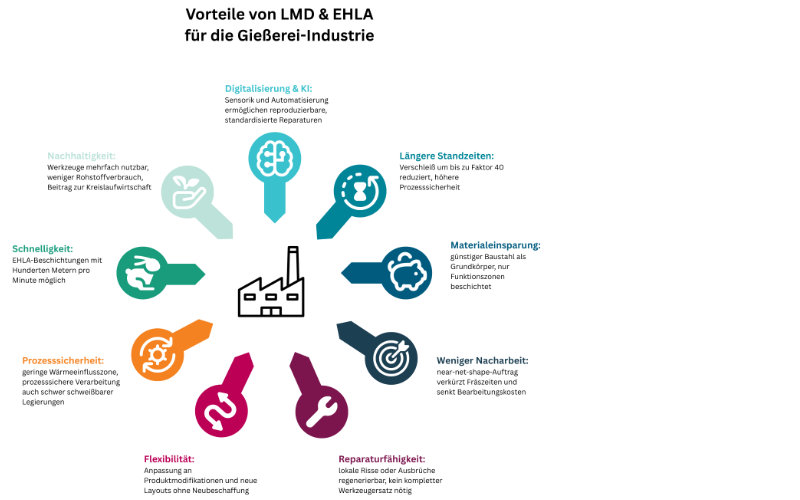
The benefits of LMD and EHLA for the foundry industry are numerous and extend far beyond simply extending tool life. The process offers clear economic and technical advantages, particularly for die-casting molds that are exposed to extreme temperature fluctuations and abrasive wear. Current research shows that targeted coating of functional zones can significantly reduce wear-induced material removal. In sliding friction wear tests, improvements of up to a factor of 40 were observed compared to conventional tool steel, depending on the selected alloy and process parameters. Materials such as a high-alloy carbide-forming material achieve hardnesses of up to 930 HV while maintaining a bond with the base material. These results impressively demonstrate that tool life can be significantly extended, which has a direct impact on production reliability and cost-effectiveness.
In addition to extending tool life, LMD enables a more efficient use of materials. While conventional tools are often made entirely of expensive, high-alloy tool steel, the use of LMD allows for the use of a cost-effective structural steel as a substrate. Only the areas that are actually exposed to high stresses are coated with a hard alloy. This “material-on-demand” principle not only reduces costs but also minimizes machining requirements. The near-net-shape deposition eliminates a large portion of the time-consuming milling operations, and molds can be put into service more quickly. Tools that previously had to be completely replaced after cracks or spalling occurred can now be remanufactured using LMD. Damaged areas are selectively rewelded and then machined so that the tools regain their original geometry. This capability not only offers potential cost savings but also reduces dependence on long supply chains for new molds. This flexibility is a decisive factor, particularly for large and complex die-casting tools that require customized manufacturing processes.
AI-SLAM: Automated Repair Using Artificial Intelligence
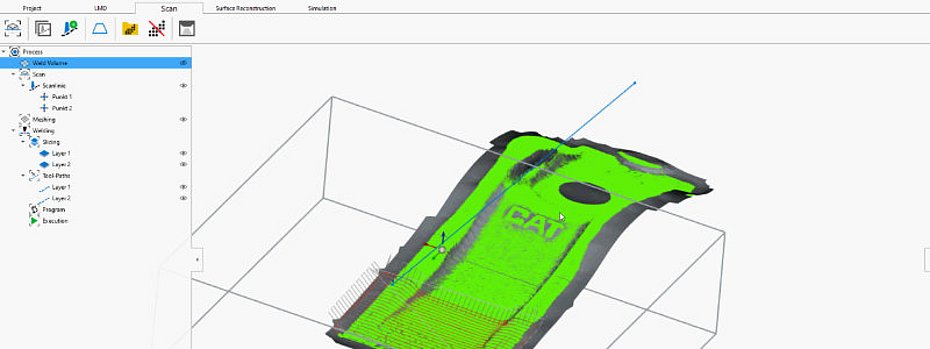
A crucial step toward the series application of laser material deposition in toolmaking is increasing automation. In the AI-SLAM (Artificial Intelligence Enhancement of Process Sensing for Adaptive Laser Additive Manufacturing) research project, experts at Fraunhofer ILT, in collaboration with international partners, have demonstrated that coating and repair processes can be automated using sensor technology and artificial intelligence. In the AI-SLAM project, a line laser equipped with a camera scans the worn surface of a tool for the mining industry and compares it with the original CAD geometry. Based on the difference, the software calculates the exact travel paths and the required layer thickness to restore the original contour. Path planning is performed automatically, and the AI monitors the process even while the job is in progress. Deviations in the size or characteristics of the molten pool or in the geometry are immediately detected and corrected by adjusting the process parameters.
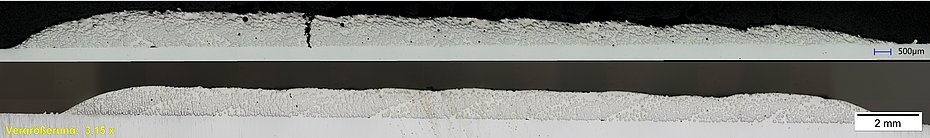
One distinctive feature is the wide range of monitored parameters. In addition to geometry, pyrometers measure temperature, cameras analyze the shape of the melt bath, and profilometers monitor the layer structure. These data streams are consolidated in real time and evaluated by AI. Operators no longer need to manually adjust complex parameters; they simply need to issue the start command, and the system takes over control of the process. This reduces the reliance on highly specialized personnel, who were previously indispensable for the successful use of LMD. This also represents a significant advance for the foundry industry. Repairs to die-casting molds—which previously required extensive planning and a great deal of experience to carry out—can now be performed in a reproducible and standardized manner. Of particular interest is the ability to automatically regenerate even large and complex molds. Defects are not only detected but also immediately corrected, drastically reducing downtime. In addition, the results can be documented and verified, which is essential for series production in an industrial setting. The AI-SLAM project opens up a new perspective in which tools are no longer viewed as wear parts but rather as long-lasting investments that can be optimized and improved throughout their entire lifecycle.
An Innovative Approach to the Manufacture of Forming Tools
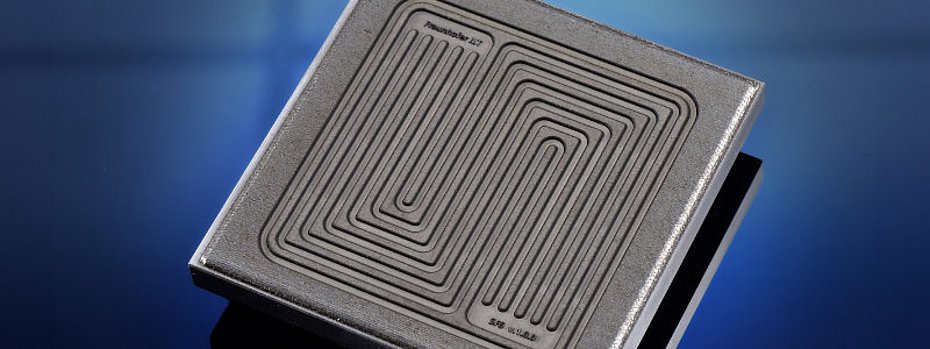
As part of the H2GO project (National Action Plan for Fuel Cell Production), the Fraunhofer ILT has presented a novel approach to the manufacture of forming tools for bipolar plates. Instead of milling tools from solid stock—a time- and material-intensive process—a wear-resistant functional layer is applied directly to low-cost structural steel using EHLA. This method produces tools faster, more cost-effectively, and with significantly less material usage. The coating materials used include high-speed steel 1.3343 and Ferro55, which achieve hardness values of up to 865 HV0.5. A typical EHLA application produces a layer thickness of approximately 0.05 mm to 0.15 mm per layer; the required final contour can be precisely built up by applying multiple layers. The process not only saves milling time, tools, and material costs but also increases the service life of the manufactured molds. A demonstrator clearly illustrated the entire process: from EHLA coating through finishing to the structuring of functional surfaces using ultrashort-pulse lasers. In cooperation with the Fraunhofer IPT, the tools manufactured in this way are currently being tested under realistic conditions. The goal is to validate the service life of the EHLA-coated tools under industrial stress scenarios.
One key advantage is already apparent: The process allows for the application of particularly hard, long-term stable alloys to the tool surface—alloys that are difficult or nearly impossible to machine using conventional methods. This significantly increases the service life of the tools, which directly contributes to lower production costs. In addition, EHLA enables localized application: Defective or worn areas can be repaired in a targeted manner, allowing tools to be reused multiple times. This potential for reuse represents another promising avenue for cost reduction and also opens up new possibilities for toolmaking in other industries. “Applying these approaches to the foundry industry can revolutionize existing processes in toolmaking,” Thomas Schopphoven is certain. “Instead of procuring new molds in fixed cycles, companies can use their existing tools longer and more efficiently.” At the same time, LMD opens up the possibility of continuously adapting tools to new product designs and manufacturing requirements. In an era where flexibility and speed, resilience, and independence from supply chains represent decisive competitive advantages, laser cladding is becoming a key technology for the future of toolmaking. (OM-11/26)
Contact
Fraunhofer Institute for Laser Technology ILT
Steinbachstraße 15
52074 Aachen (Germany)
Phone: +49 241 8906-194
Email: info@ilt.fraunhofer.de
www.ilt.fraunhofer.de
About Fraunhofer ILT
The Fraunhofer Institute for Laser Technology ILT is one of the world’s leading contract research and development institutes in its field. Under one roof, the Fraunhofer Institute for Laser Technology ILT offers research and development, system integration and quality assurance, consulting, and training. To carry out research and development projects, the institute has access to numerous industrial laser systems from various manufacturers as well as an extensive infrastructure.